Application engineering
UV adhesives & fast curing
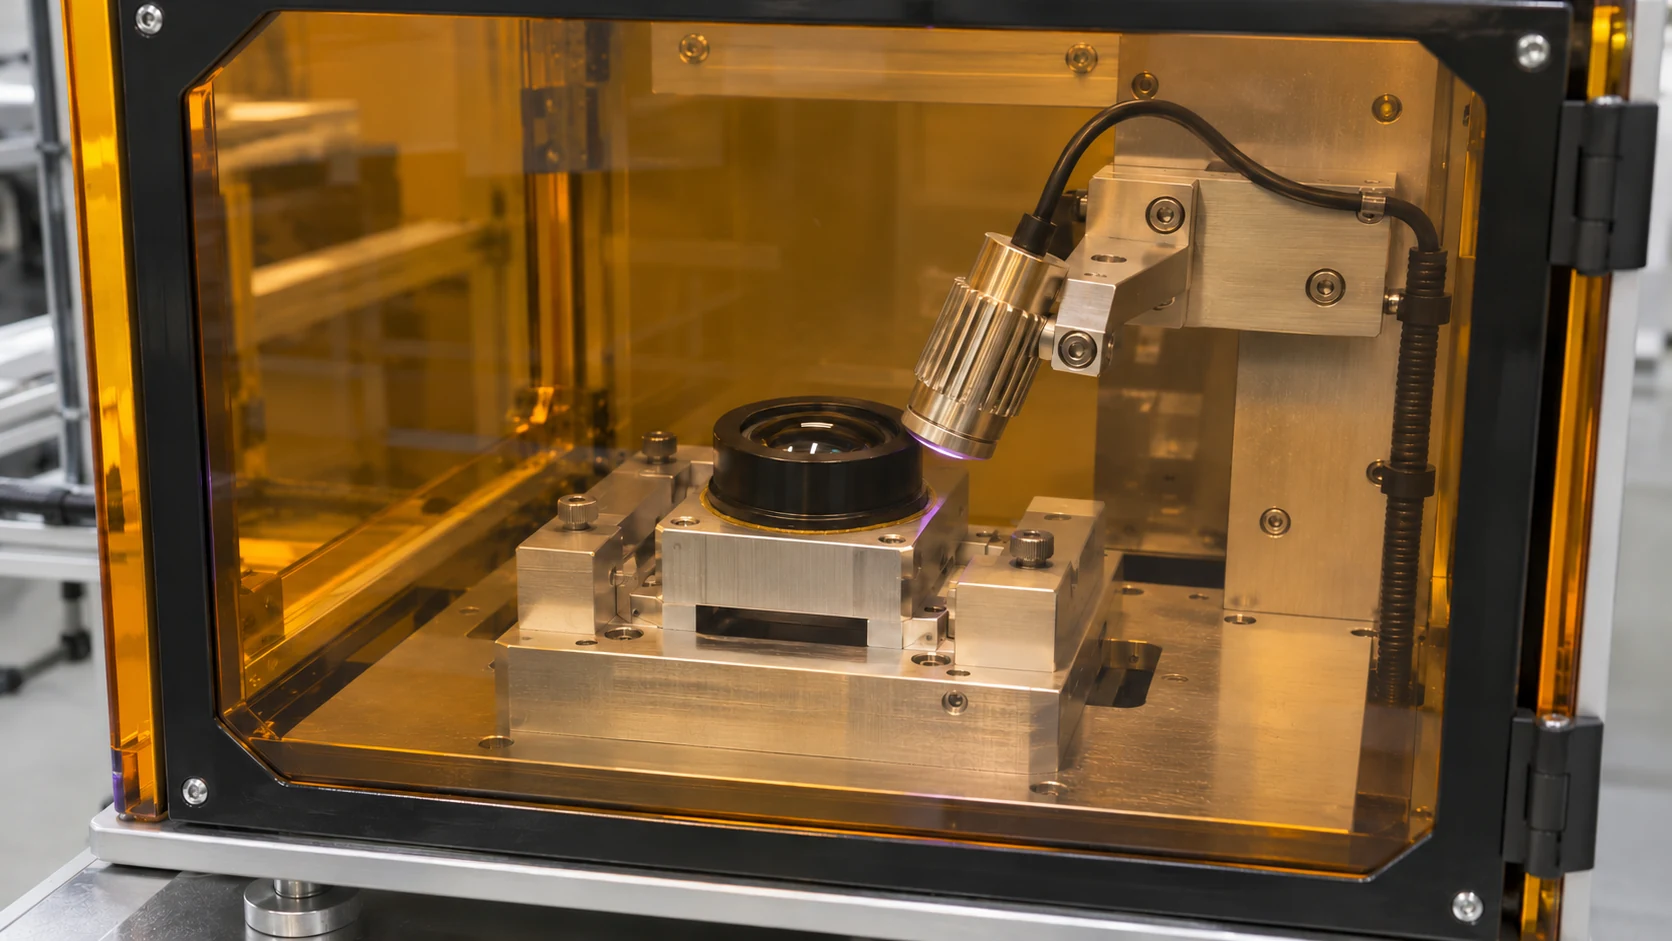
Light-curable adhesives can support short assembly sequences when the material and joint allow an effective cure. Dispensing and exposure therefore need to be developed together. We engineer the deposit location, part support and access for the curing head, with shielding and machine controls included in the station. Where parts obscure the bond line, the material choice and curing strategy must account for those shadowed regions.
Placement and part location
The valve, tip and fixture are selected for the bond geometry. Dispense amount and the movement into assembly are coordinated so the adhesive reaches the intended interface while the parts remain located during the next operation.
Light delivery at the bond
Curing-head position, wavelength and exposure are developed for the adhesive and available light path. Trials establish the practical arrangement; opaque features may call for another exposure position or a suitable secondary-cure chemistry.
Guarding and machine timing
Shielding, interlocks and exposure timing are integrated with the dispense and handling sequence. The equipment can combine these operations in one station or transfer the part to a separate guarded curing position.